English
 日本語
 한국어
 français
 Deutsch
 Español
 русский
 português
 العربية
 tiếng việt
 ไทย
Products
Silanes & Catalysts
Silicone Fluids & Reactive Polymers
Silicone Resin
Silicone Rubber
Silicone Surfactant
Conformal Coating
Fluorinated Electronic Coating
Phenyl Silane & Siloxane
Fluoro Silane & Siloxane
Silane Oligomers & Waterborne Silanes
Alpha Silanes
Amino Silanes
Customized Silane
Crosslinkers, Latent Silanes & Catalysts
Polyolefin Catalysts & Donors
Siloxanes & Silazane
Alkoxy Silicone Fluid
Hydrogen Silicone Oil
Silanol Sillicone Fluids & OH Polymer
Regular Silicone Fluid
Phenyl Silicone Fluid
Fluorosilicone Fluid
Vinyl Silicone Fluid
MQ Silicone Resin
LR-021 Organic Silicone Resin
LR-030 Silicone Resin
LR-037 Solvent Free Silicone Resin
LR-038 Solvent Free Methyl Phenyl Silicone Resin
LR-131 Solvent Free Silicone Resin
LR-152 Organic Silicone Resin
LR-160 Silicone Resin for Heat-resistant Coating
LR-162 Methyl Phenyl Silicone Resin
LR-163 Methyl Phenyl Silicone Resin
LR-240/241/242 Solid Silicone Resin
LR-608 Methyl Silicone Resin
LR-E168 Methyl Phenyl Silicone Resin Emulsion
LR-E169 Silicone Resin Emulsion
LR-E212 Silicone Resin Emulsion
LR-EP167 Silicone Resin Emulsion
LR-H160 High Resistant Silicone Resin
LR-H161 Heat Resisitant Air-drying Silicone Resin
LR-H167 High Resistant Silicone Resin
LR-H168 High Resistant Silicone Resin
LR-M123 Epoxy Modified Silicone Resin
LR-M124 Acrylic Modified Organic Silicone Resin
LR-M125 Alkyd Modified Silicone Resin
LR-M161 Polyester Modified Organic Silicone Resin
LR-M163 Acrylic Modified Silicone Resin
LR-M164 Epoxy-modified Silicone Resin
LR-S161 Heat Resistant Air-drying Silicone Resin
LR-S164 Air Drying Silicone Resin
LR-TMP10 Solid Silicone Intermediate
LR-610 Polymethylsilsesquioxane(PMSQ)
LA-10 Agricultural Silicone Surfactant Polyether-Modified Trisiloxane
LA-11 Agricultural Silicone Penetrant Polyether-Modified Trisiloxane Agricultural Surfactant
LA-12 Agricultural Organosilicone Adjuvant
LA-13 Oil Soluble Agricultural Silicone Adjuvant Alkyl-Modified Trisiloxane
LA-14 Agricultural Silicone Spreading Agent Polyether-Modified Trisiloxane
LA-15 Agricultural Silicone Surfactant Polyalkyleneoxide Modified Trisiloxane
LA-ST493 Polyether-Modified Polysiloxane Silicone Surfactant
LS-653 Phenyl Siloxane
LS-P60 Phenyl Siloxane
LS-M11 Phenyltrimethoxysilane
LS-E11 Phenyltriethoxysilane (Donor A)
LS-M12 Diphenyldimethoxysilane
LS-E12 Diphenyldiethoxysilane
LS-M13 Dimethoxymethylphenylsilane
LS-M14 Methoxytriphenylsilane
LS-H12 Dihydroxydiphenylsilane
LS-H13 Triphenylsilanol; Hydroxytriphenylsilane
LS-614 Hexaphenyldisiloxane
LS-615 1,1,5,5-Tetramethyl-3,3-Diphenyl-Trisiloxane
LS-618 Octaphenylcyclotetrasiloxane
LS-6345 Methylphenylcyclosiloxane
LS-M121 Methyldiphenylmethoxysilane
LS-PHIPS Phenyltris(isopropenyloxy)silane
LS-644 Tetraphenyltetramethyltrisiloxane
LS-532 (3,3,3-Trifluoropropyl) Dichloromethylsilane
LS-533 Tridecafluorooctyl) Trichlorosilane
LS-M531 3,3,3-Trifluoropropyl) Methyldimethoxysilane
LS-M53 3,3,3-Trifluoropropyltrimethoxysilane
LS-M59 1H,1H,2H,2H-Nonafluorohexyltrimethoxysilane
LS-E59 1H,1H,2H,2H-Nonafluorohexyltriethoxysilane
LS-M513 1H,1H,2H,2H-Perfluorooctyltrimethoxysilane
LS-E513 1H,1H,2H,2H-Perfluorooctyltriethoxysilane
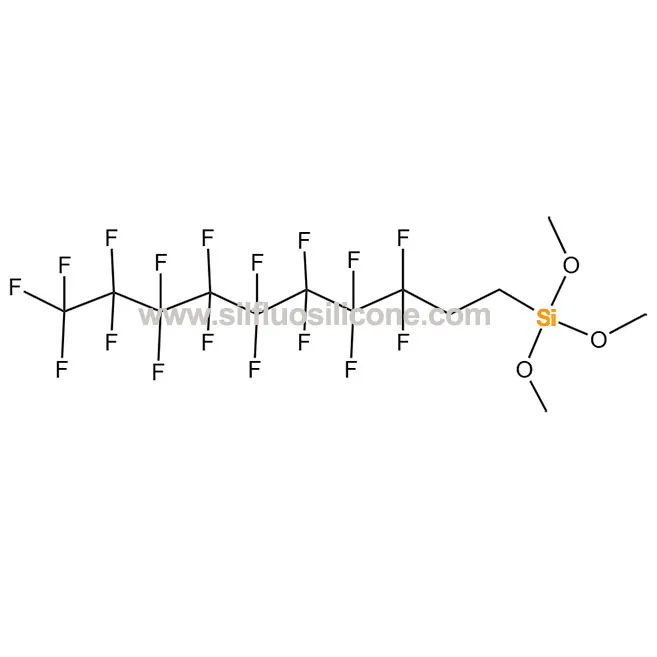
LS-M517 1H,1H,2H,2H-Perfluorodecyltrimethoxysilane
LS-E517 1H,1H,2H,2H-Perfluorodecyltriethoxysilane
LS-51 2,2,2-Trifluoroethyl Methacrylate
LS-52 1H,1H,2H,2H-Perfluorodecanethiol
LS-651 1,3,5-Tris [ (3,3,3-Trifluoropropyl) Methyl] Cyclotrisiloxane/D3F
LS-M512 Dodecafluoroheptylpropyltrimethoxysilane
LS-53C Perfluoropolyether Modified Acrylic Compound PFPE Modified Acrylic Compound
LS-O146 Oligomeric Diamino Functional Silane
LS-O110 Aqueous 3-aminopropylsilane Hydrolysate
LS-OL310 N-Octyltrimethoxysilane Oligomer
LS-OL320 N-Octyltriethoxysilane Oligomer
LS-OP121 Methylphenyldimethoxysilane Oligomer
LS-OP200 Epoxy Silane Oligomer
LS-E85 Methacryloxymethyltriethoxysilane
LS-E86 N-(3-(Triethoxysilyl)methyl)butylamine
LS-E87 N-[(Triethoxysilyl)methyl]cyclohexylamine
LS-E88 2-aminoethylamine Methyl Triethoxysilane
LS-ND22 Diethylaminomethyltriethoxysilane
LS-ND42 (N-Phenylamino)methyltriethoxysilane
LS-ND43 Dichloromethyltriethoxysilane
LS-8121 Chloromethyl(dimethoxy)methylsilane
LS-AM31 Methyl n-(trimethoxysilylmethyl)carbamate
LS-AM121 Methyl [n-(dimethoxymethyl)silylmethyl]carbamate
LS-MA131 Acryloyloxymethyltrimethoxysilane
LS-A431 N-(3-(Trimethoxysilyl)propyl)butylamine
LS-AB31 N-Phenyl-gamma-aminopropyltrimethoxysilane
LS-AD31 Bis(trimethoxysilylpropyl)amine 1170
LS-AD323 Bis[3-(triethoxysilyl)propyl]amine 1171
LS-AV31 γ-Aminopropyl-N-cyclohexylmethyldimethoxysilane 1130
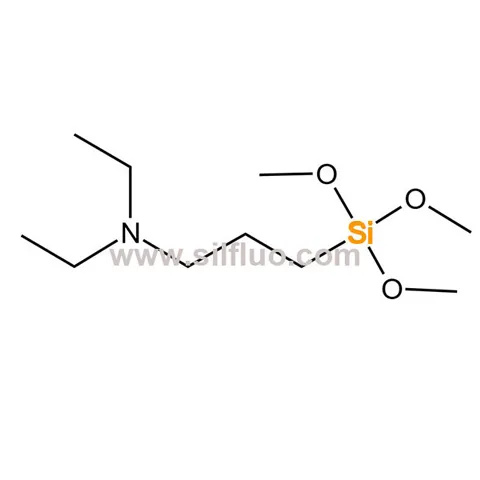
LS-M81 3-(Diethylamino)propyltrimethoxysilane
LS-AH13 N-(6-aminohexyl)aminomethyltriethoxysilane
LS-AS32 N-[3-(triethoxysilyl)propyl]-4,5-dihydroimidazole
LS-AS213 2,2-Dimethoxy-1-[3-(trimethoxysilyl)propyl]-1,2-azasilolidine
LS-B632 Benzylsilane Vinylbenzylaminoethylaminopropyltrimethoxysilane
LS-B6032 Benzylsilane 3-(N-Styrylmethyl-2-aminoethylamino)-propyltrimethoxysilane
LS-B6224 Vinylbenzylaminofunctionaltrimethoxysilane
LS-D312 1,2-Bis(trimethoxysilyl)ethane
LS-D322 1,2-Bis(triethoxysilyl)ethane
LS-A112T (2-Aminoethyl)-3-aminopropyltrimethoxysilane (Technical Grade)
LS-94322 1,1,3,3-Tetramethyl-1-[2'-(Trimethoxysilyl)Ethyl]-Disiloxane
LS-VI33 VTIPOS Vinyltriisopropoxysilane
LS-AMS Allyltrimethoxysilane
LS-GLYDME 3-(Glycidyloxy)propyldimethylethoxysilane
LS-M304 (3-Acryloxypropyl)trimethoxysilane
LS-OP594 3-Methacryloxypropyletris(trimethylsiloxy)silane
LS-BSA N,O-Bis(trimethylsilyl)acetamide(BSA)
LS-PEG20 3-[Methoxy(Polyethyleneoxy)-Propyl]Trimethoxysilane
LS-VTPS Vinyltris(tert-butylperoxy)silane
LS-AS312 3-(1,3-dimethylbutylidene)aminopropylmethyldiethoxysilane
LS-AS332 3-(1,3-dimethylbutylidene)aminopropyltriethoxysilane
LS-AT102 Methyltriacetoxysilane
LS-AT402 Ethyltriacetoxysilane
LS-MITS 3-methacryloxypropyltri(isopropenyloxy)silane
LS-MMOS Methyimethoxybis(methylethylketoximino)silane
LS-MVOS Vinylmethylbis(methylethylketoximino)silane
LS-VIPS Vinyltriisopropenoxysilane
LS-GCF 1,1,3,3-Tetramethyl-2-[3-(Trimethoxysilyl)Propyl]Guanidine
LF-EH101 Methyl Hydrogen Polysiloxane Emulsion
LF-H101H High Hydrogen Silicone Fluid
LF-H101L Low Hydrogen Silicone Fluid
LF-H101S Side-H Silicone Oil
LF-H101T Terminal-H Silicone Oil
LF-H101TS Terminal & Side-H Silicone Oil
LF-OHP Silanol Terminated Polydimethylsiloxane
LF-OHP2 Diphenyl Hydroxy Silicone Oil
LF-OHPM Phenyl Methyl Hydroxy Silicone Oil
LF-OHPV Vinyl Hydroxy Silicone Oil
LF-201 Dimethyl Silicone Fluid
LF-211 Low-Viscosity Dimethyl Silicone Fluid
LF-221 High-Viscosity Dimethyl Silicone Fluid
LF-AM11 Long Chain Alkyl-Modified Silicone Fluid
LF-PM12 Diphenyl Silicone Oil
LF-PM13 Phenyl Siloxane
LF-PM11 Phenylmethyl Silicone Fluid
LF-PV11 Phenylvinyl Silicone Fluid
LF-PH11 Phenyl Hydrogen Silicone Fluid
LR-MQ Liquid Methyl MQ Silicone Resin
LR-MQ Powder Methyl MQ Silicone Resin
LR-MQP Vinyl phenyl Silicone M/Q Resin
LR-MQPH Phenyl Hydrogen Silicone Resin
LR-MQV Liquid Methyl Vinyl MQ Silicone Resin
LR-MQV Powder Vinyl-Functional MQ Silicone Resin
LR-TMS Silicone MQ Resin
LR-F5100 Fluoro Silicone Gum
LR-F5200 High Tear Strength Series Fluorosilicone Rubber
LR-F5300 Low Pressure Deformation Fluorosilicone Compound
LR-F5400 High Resilience Series Fluorosilicone Rubber
LR-F5500 Adhesive Purpose Series Fluorosilicone Rubber
LR-F5502 Adhesive Purpose Series Fluorosilicone Rubber
LR-F5600 Flame-retarded Series Fluorosilicone Rubber
LR-F5700 Extruded Fluorosilicone Rubber